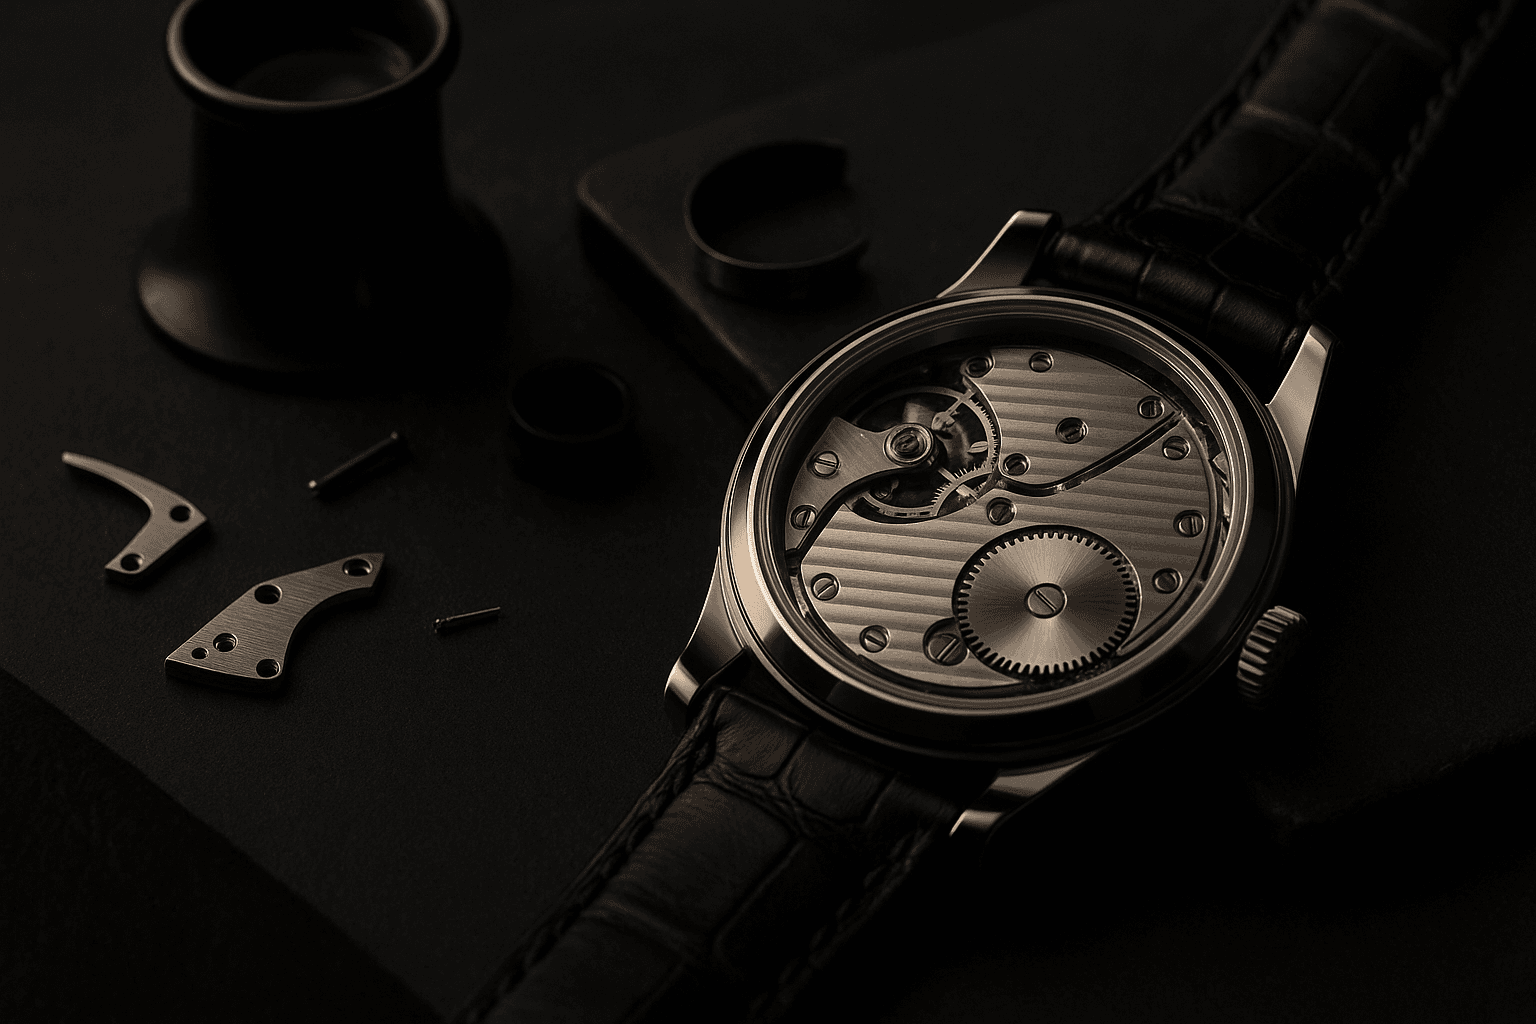
What Hand-Finishing Costs: Reading Anglage, Black Polish, and Côtes de Genève Before You Pay the Premium
By The Subdial Editors ·
Can you tell, through a 10x loupe, whether the bevel running along the edge of a bridge was cut by a rotating tool or shaped by hand with a file and a stick of gentian wood? Most buyers cannot, and a meaningful share of the five-figure price differences in high-end watchmaking rests on exactly that gap.
Finishing is the one line in a mechanical watch's cost structure that is almost entirely labor and almost entirely invisible from arm's length. It is also the line brands describe in the vaguest possible language, because vagueness is commercially useful.
What follows is a working guide to reading a movement the way a finisseur reads it. We separate the operations a machine completes in minutes from the ones that still consume a skilled hand for hours, and attach defensible cost ranges to each.
What are you paying for when a movement is called hand-finished?
Hours of skilled labor, not materials. Hand anglage, black polish and hand engraving run hours per part, while Côtes de Genève and perlage are machine operations measured in minutes.
What "Hand-Finished" Actually Means
Unlike "Swiss made," which is defined by federal ordinance, the phrase "hand-finished" carries no regulated meaning whatsoever. A brand may apply it to a movement whose bevels were cut on a five-axis machine and whose only hand operation was a final pass with a polishing stick.
This is why the useful question is never whether a movement is hand-finished. The useful question is which specific operations were hand-executed, on which parts, and whether the work extends to surfaces the owner will never see.
Finishing divides cleanly into three cost classes once you stop reading marketing copy. Surface decoration is inexpensive, edge work is expensive, and specular polishing on steel sits between the two but much closer to the expensive end.
Anglage: The Operation A Machine Still Cannot Fake
Anglage is the bevel, usually cut at roughly 45 degrees, running along the edges of bridges, levers, springs and wheel spokes. Its original function was practical, since a chamfered edge sheds the burrs that would otherwise break loose and circulate through the gear train.
A CNC machine produces a bevel very capably along a straight run or a gentle curve. What it cannot produce is a sharp interior angle, because every rotating cutter has a radius and leaves a small fillet wherever the edge turns inward.
That limitation is the single most reliable test available to a buyer holding a loupe. Find a bridge outline that turns back on itself — an inward corner, sometimes called a re-entrant angle — and look closely at the point of the turn.
A machine-cut corner shows a visible rounding, a small curve where the bevel changes direction. A hand-filed corner comes to a point, because the finisseur worked into the corner with the edge of a file and then burnished the facet flat.
How do you tell hand anglage from machine anglage?
Look at the inward corners. Every rotating cutter leaves a small radius, so a sharp, pointed interior angle at 10x is the clearest evidence that a hand file and burnisher did the work.
The second tell is the profile of the bevel itself. Hand anglage presents a flat facet bounded by two crisp lines, whereas a machined and tumbled edge tends to look rolled, blending softly into the top surface without a defined boundary.
The third tell is where the work stops. Many movements carry respectable anglage on the upper bridges and none at all on the dial-side plate, on the undersides of bridges, or on the spokes of the wheels.
Time is the reason for all of this. Estimates circulated by independent makers and finishing-school curricula commonly put a single complex bridge at several hours of anglage alone, which is why a fully hand-angled calibre can absorb thirty to sixty hours or more before assembly even begins.
The extremes live with the small independents rather than the industrial houses. Our coverage of Voutilainen and Akrivia as collector-grade independents and of Greubel Forsey's production economics traces the same pattern, where finishing hours rather than complications set the ceiling on annual output.
Black Polish: Flatness You Measure With Light
Black polish, also called poli noir or specular polishing, is the process of lapping a steel part flat enough that it reflects incident light in a single direction. Held at one angle it appears mirror-bright, and rotated a few degrees it goes solid black.
The traditional method is a plate of zinc or tin charged with diamantine paste, with the part worked across it in a figure-eight so no groove is cut into the plate. Flat and accessible surfaces — a click spring, a chronograph bridge, a cap over an escape wheel — can now be lapped semi-automatically on modern equipment.
Curved, small or three-dimensional steel parts remain stubbornly manual. A black-polished, bevelled steel lever with a domed upper surface is among the most expensive square millimeters in watchmaking, because the operator has to hold flatness across a geometry that resists it.
How do you spot true black polish?
Tilt the part under a single light source. A truly lapped surface flips from mirror-bright to solid black as the angle changes, while a merely polished surface stays uniformly shiny from every direction.
Be aware that photography conceals this almost perfectly. A studio image lit diffusely makes any polished steel read as black polish, which is why the test only works with a point source and a part you can rotate in your hand.
Côtes De Genève, Perlage, And The Decoration That Costs Almost Nothing
Côtes de Genève — the parallel bands sweeping across the bridges — is applied by a rotating abrasive peg on a machine, in a pass measured in minutes. Perlage, the field of overlapping circular graining on the mainplate, is produced the same way with a different tool.
Both are handsome, both are traditional, and neither is expensive. That combination is precisely why marketing departments lean on them so hard, since they photograph beautifully and appear on movements at nearly every price point in the market.
There is a genuine quality spread within striping, and it is worth learning. Stripe pitch consistency, whether the bands align across adjacent bridges, and whether the stripe edges are clean rather than furred all separate careful machine work from careless machine work.
Keep in mind that sequence matters more than pattern here. On well-made movements the striping is applied first and the bevel cut afterward, so the stripe terminates in a crisp line at the top edge of the bevel; on cheaper work the bevel comes first and the striping pass leaves a faint burr hanging over the edge.
Is Côtes de Genève a marker of high-end finishing?
On its own, no. Geneva stripes are machine-applied in minutes and appear at nearly every price point, which makes them the most visible and least costly decoration on a movement.
Hand Engraving And The Finishes That Cannot Be Duplicated
Hand engraving occupies a category of its own, since the output varies from piece to piece by definition. The balance cock on every A. Lange & Söhne movement is engraved individually by hand, which is why the floral pattern differs subtly between two examples of the same reference.
Frosted and grained plate treatments belong in the same discussion. German silver left untreated, as Lange uses it, develops a patina across years of ownership that a rhodium-plated brass plate never will — a finishing decision with a maintenance consequence attached to it, as our Saxonia Thin collecting guide sets out.
The Three-Tier Finishing Ladder
Once the individual operations are separated, movements sort into three broad tiers. The boundaries are not official, but they track closely with what a buyer can actually verify at 10x.
| Tier | What you see at 10x | Typical execution |
|---|---|---|
| Industrial decorated | Machine stripes and perlage, rolled bevels or none, unpolished countersinks, plain screw heads | Fully automated decoration |
| Hybrid high-industrial | Clean machine bevels with hand-corrected corners, polished countersinks, a handful of black-polished steel parts, dial side left plain | CNC base with selective hand passes |
| Fully hand-finished | Sharp interior angles, flat faceted bevels of even width, black polish across the steel, finishing continued on dial-side and hidden surfaces | Hand execution throughout |
Most of what the market calls haute horlogerie sits in the middle tier, and that is not a criticism. It is simply the tier where the price and the labor content are most often misaligned with the language used to describe them.
What Each Operation Costs To Produce
Direct labor is the honest way to price finishing, and pricing it requires an hourly figure. Fully-loaded bench cost for a skilled Swiss finisseur is commonly estimated in the range of roughly CHF 60 to CHF 120 per hour, a range we treat as an estimate because brands do not publish it.
| Operation | How it is executed | Estimated time per movement | Cost weight |
|---|---|---|---|
| Côtes de Genève | Rotating abrasive peg, machine-guided | Well under one hour | Low |
| Perlage on the mainplate | Semi-automatic, hand-guided | Well under one hour | Low |
| Circular graining on wheels | Machine | Minutes | Low |
| Machined bevel (rolled edge) | Included in the CNC machining pass | No added bench time | Negligible |
| Polished countersinks and jewel sinks | Hand or semi-automatic | Roughly one to several hours | Moderate |
| Hand anglage with sharp interior angles | File, burnisher, gentian wood and diamantine | Several hours per bridge; commonly 30 to 60+ hours in total | Very high |
| Black polish on steel parts | Hand-lapped on zinc or tin with diamantine | Roughly 30 minutes to several hours per part | High |
| Hand engraving (balance cock) | Hand graver | Hours per piece | High |
Note that the time figures above are estimates drawn from independent makers' public statements and finishing-school curricula, not from disclosed manufacturing data. Verify against a brand's own statements where they exist before treating any of them as precise.
Applied to a fully hand-angled and black-polished movement absorbing thirty to sixty hours, that arithmetic lands somewhere between roughly CHF 2,000 and CHF 7,000 in direct finishing labor. Machine decoration on the same movement would represent a small fraction of a single hour within that total.
Then the distribution multiplier applies. Traditional Swiss distribution has historically carried an ex-works to retail multiple estimated in the region of 2.5x to 3.5x, with brand-owned boutique channels compressing it, which is how several thousand francs of bench time becomes a five-figure difference on a price list.
Does the hand-finishing premium reflect real cost?
Partly. Thirty to sixty hours of bench work at an estimated CHF 60 to 120 per hour is genuine cost, and the remainder of the premium is priced by the scarcity of finisseurs who can execute it.
All of this adds up to a defensible premium and an indefensible one sitting side by side on the same invoice. The labor arithmetic supports a substantial number, and what sits above it is priced by how few people can execute a sharp interior angle consistently — a population small enough that the leading independents quote waiting lists in years rather than months.
A Loupe Protocol You Can Run At The Counter
Evaluation takes about two minutes once you know the sequence to follow. Use a 10x loupe, since 5x hides the corners entirely and anything above 15x exaggerates flaws that no movement on earth is built to survive.
Here's the order to work in:
- Interior angles first. Find an inward corner on a bridge outline and look for a point rather than a radius. This one check separates hand from machine faster than everything else combined.
- Then the bevel profile. A flat facet with two crisp boundary lines indicates hand work, while a soft rolled edge that blends into the top surface indicates a machined and tumbled edge.
- Then the countersinks. Every jewel and screw hole sits in a chamfered recess. On careful work that recess is polished and its rim is a clean circle; on industrial work it retains machining marks and a slightly ragged rim.
- Then the screws. Look for polished heads, bevelled slot edges and bevelled rims. Sharp, unpolished slot edges tell you the finishing budget ran out before it reached the fasteners.
- Then the wheels. Check whether the spokes are bevelled and polished on their inner edges, and whether circular graining covers the upper faces. Wheel finishing is expensive and is frequently the first thing skipped.
- Then the light test. Tilt the movement under a single point source and watch for steel parts that flip from bright to black. Diffuse boutique lighting will defeat this, so angle away from it.
- Finally, the hidden surfaces. Ask whether the dial-side plate and the undersides of the bridges are finished. This is where finishing budgets are quietly cut, and where the serious makers refuse to cut them.
Working through that sequence gives you a defensible read on labor content without any reliance on what the brand claims. Remember that you are not grading beauty here — you are counting operations that had to be paid for by the hour.
How do you know a brand finished more than the visible surfaces?
Ask to see the dial side. Movements finished only where the display back shows carry plain machined plates underneath, while fully finished calibres carry bevels and graining throughout.
Where Certifications Help, And Where They Stop
Three certifications intersect with finishing, and each is narrower than its reputation suggests. Note that all three prescribe standards the finished work must meet rather than the method by which it was produced.
The Poinçon de Genève, established in 1886 and administered today by Timelab, requires that the movement be assembled, adjusted and cased within the Canton of Geneva, and it sets criteria covering bevelled and polished steel parts, drawn flanks, polished screw heads with bevelled slots, and wheel finishing. Its 2011 revision extended the hallmark from the movement to the complete watch and added functional and rate testing, and our Vacheron Constantin collecting guide covers which references carry it.
Qualité Fleurier, launched in 2004 by Chopard, Parmigiani Fleurier, Bovet and Vaucher, layers a chronometer requirement, the Chronofiable ageing protocol and the Fleuritest wear simulation on top of finishing criteria and a fully Swiss manufacturing requirement. Our Chopard L.U.C collecting guide maps that certification onto the calibres that hold it.
The Patek Philippe Seal, introduced in 2009 when the brand withdrew from the Geneva hallmark, is administered internally and covers the complete watch including rate tolerances. Independent third-party verification is not part of that arrangement, a distinction worth understanding alongside the reality of Patek allocation.
All of these raise the floor, and raising the floor has real value. None of them certifies that a given bevel was filed by hand rather than cut by a machine, which is exactly why the loupe test remains the operative one.
Does Any Of It Do Anything Functional?
The functional case for finishing is real but narrow, and it deserves to be stated accurately. Chamfering removes burrs that could break free and contaminate the lubricant, polished pivots and cleanly finished wheel teeth reduce friction, and a polished surface presents fewer nucleation sites for corrosion than a rough one.
Beyond that, decoration remains decoration. Chronometric performance comes from escapement geometry, the hairspring, the poising of the balance and the quality of regulation, and a movement can run to exceptional tolerances with no anglage at all — as industrial chronometry has demonstrated for the better part of a century.
The honest framing is that hand-finishing is craft you buy because you value craft. Grand Seiko makes the same argument on the outside of the watch, where Zaratsu polishing produces a distortion-free flat surface through labor rather than through engineering necessity.
What The Secondary Market Actually Pays For
Finishing supports resale value reliably only when it is attached to a name the market can already price. A superbly finished movement inside a brand with thin secondary demand recovers very little, because the buyer at the other end prices the maker first and the calibre second.
Where the maker is established, finishing becomes the evidence that sustains the premium rather than the premium itself. Our analysis of value retention across the market and of the F.P. Journe premium both show finishing functioning as proof-of-work behind a scarcity story.
Keep in mind that finishing carries a service cost as well. Refinishing to original standard after a service is rarely achievable outside the manufacturer, which is one of the practical constraints covered in the ownership economics of high-end watches and in our reporting on parts access across the industry.
Editorial recommendation
If finishing is what you are paying for, buy against verifiable operations rather than against language:
- Require sharp interior angles. Treat their absence as evidence that the bevels were machined, regardless of how the movement is described in the catalogue.
- Require finishing on hidden surfaces. Dial-side bevels and grained undersides are the cheapest signal that a maker did not optimize for the display back alone.
- Treat striping and perlage as neutral. Grade them on execution quality, and give them no weight at all in the price you are willing to pay.
- Ask which parts are black polished, by name. A specific answer indicates the operation was budgeted; a general one indicates it was not.
- Buy the maker first, the finishing second. Finishing quality defends a premium the market already recognizes far more effectively than it creates one from nothing.
Frequently Asked Questions
How can you tell if anglage was done by hand?
Look for sharp interior angles. A rotating tool always leaves a small radius in an inward corner, so a crisp re-entrant angle under a 10x loupe is the clearest available evidence of hand filing and burnishing.
Is Côtes de Genève a sign of high-end finishing?
Rarely on its own. Geneva stripes are machine-applied in minutes on movements at almost every price point, which makes them the most visible and least expensive decoration a brand can apply.
What is black polish and how do you spot it?
It is a surface lapped flat enough to reflect light in one direction only. Tilt the part under a single light source: true black polish flips from mirror-bright to solid black as the angle changes.
Does hand-finishing make a watch more accurate?
Not directly. Rate comes from escapement geometry, the hairspring, poising and regulation, while finishing helps mainly by removing burrs that could shed debris and by polishing pivots to reduce friction.
What does the Geneva Seal actually guarantee?
A specified finishing floor plus assembly within the Canton of Geneva, and since the 2011 revision, testing of the complete watch. It prescribes standards the work must meet, not that every operation was hand-executed.
Does hand-finishing hold its value on the secondary market?
It holds value when attached to a maker the market can price. Finishing quality supports the premium on established independents, while on anonymous or weak-demand brands it rarely recovers at resale.
Before You Pay The Premium
Finishing quality is simultaneously the most checkable claim in high-end watchmaking and the least frequently checked. Two minutes with a 10x loupe, worked through in the order above, will tell you more about a movement's labor content than any amount of catalogue copy.
For reference points on how the same questions apply to specific makers and specific eras, our guides to A. Lange & Söhne finishing conventions and to movement authentication in the vintage market are the natural next reads.